E-mail: sale@xxdahan.com
Follow Us 


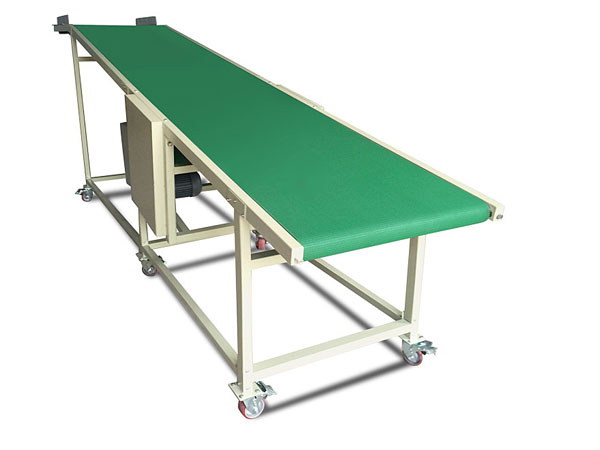
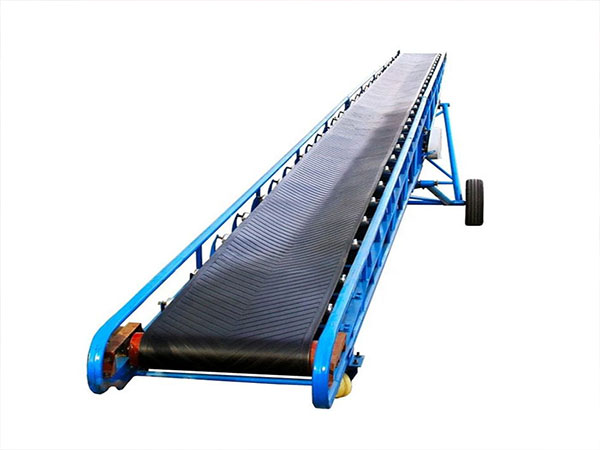
A stainless steel belt conveyor is a heavy-duty and hygienic material handling system engineered with stainless steel frames and conveying surfaces. Built to withstand corrosive environments, extreme temperatures, and strict sanitation standards, it ensures efficient, continuous product movement across industrial production lines.


Constructed primarily from premium SUS304 for general corrosion resistance or SUS316L for high-acid, saline, and pharmaceutical cleanroom environments.

Powered by a robust motor and drive pulley system, the continuous belt moves smoothly across support rollers or sliding beds, driven by friction or positive chain engagement to transport bulk or packaged goods reliably.
Every production line has unique demands. Below are the baseline technical specifications of our stainless steel belt conveyors, fully customizable to match your plant's throughput and layout requirements.
| Technical Parameter | Standard Specification Range | Customization Options |
| Material Grades | SUS304 / SUS304L | SUS316 / SUS316L (For high corrosive environments) |
| Belt Width | 200 mm – 2000 mm | Custom widths engineered to product size |
| Conveyor Length | 1,000 mm – 30,000 mm | Modular extensions available |
| Operating Temperature | -20°C to +120°C (Standard) | Up to +400°C (For high-temp baking/drying) |
| Drive System | Gear motor / Drum motor (SEW, ABB, etc.) | Variable Frequency Drive (VFD) for adjustable speed |
| Load Capacity | Up to 500 kg/m | Heavy-duty reinforced frames for high loads |
Engineered for maximum uptime and operational safety, our stainless steel belt conveyors incorporate advanced structural features tailored for demanding industrial environments.
Sanitary & Easy-to-Clean Design: Featuring seamless TIG welding, polished surfaces, and a crevice-free structure, our conveyors prevent bacterial buildup and support high-pressure washdown, fully complying with hygiene standards.
Superior Corrosion Resistance: Built with high-grade 304 or 316L stainless steel, the system resists rust, oxidation, and aggressive cleaning chemicals, ensuring long-term durability in wet or acidic workspaces.
Extreme Temperature Adaptability: Equipped with heat-resistant belts and specialized components, our conveyors perform reliably from cryogenic freezing lines to high-temperature baking and drying tunnels up to 400°C.
Low Maintenance & High Uptime: Designed with quick-release belt mechanisms, precision-aligned rollers, and sealed heavy-duty bearings to minimize manual maintenance downtime and lower operating costs.
Our stainless steel belt conveyor systems are engineered to meet the stringent sanitary, anti-corrosion, and precision demands across a wide range of global industries.
Food Processing & Packaging: Ideal for meat, seafood, bakery, and snack sorting, washing, cooling, and packaging lines. Complies strictly with food-grade safety and washdown requirements.
Pharmaceuticals & Cleanrooms: Designed for sterile tablet handling, medical device assembly, and chemical conveyance. Features zero-contamination finishes and particle-free operation.
 |
 |
Chemical & Fertilizer Handling: Built with acid- and alkali-resistant stainless steel grades to safely transport corrosive powders, granules, and chemical components without structural degradation.
Electronics & Precision Assembly: Provides stable, anti-static, and smooth transport for delicate electronic components, miniature parts, and precision-manufactured assemblies.
 |
 |
Every factory floor has unique spatial and operational constraints. Our engineering team works directly with your specifications to design a seamless, turnkey conveyor integration.
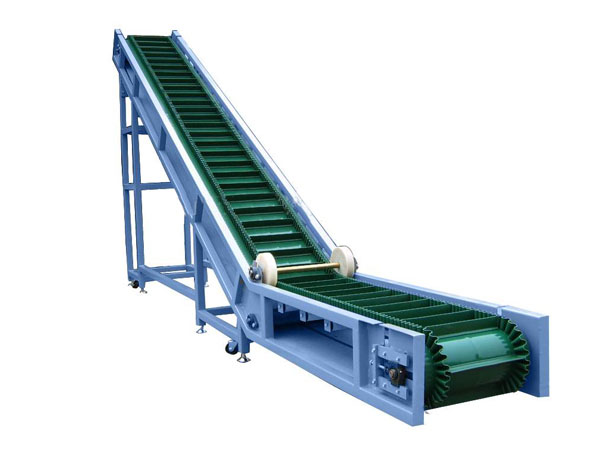
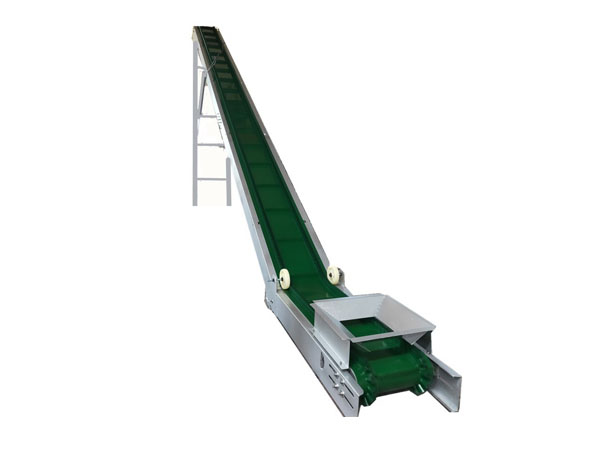
Flexible Layout Configurations: Custom-designed for horizontal runs, inclined or declined elevation changes, Z-type configurations, or curved routing to match existing production flows. Specialized Belt & Surface Accessories: Equipped with optional flight attachments, side guards, pneumatic tensioners, scraper systems, or perforated meshes for specific drainage and sorting needs. Electrical & Control Integration: Integrated control panels with VFD speed regulation, emergency stop safety chains, and PLC synchronization to interface smoothly with your master production line.

Find answers to common technical and operational questions regarding our industrial stainless steel belt conveyors.
What is the difference between SS304 and SS316 stainless steel belt conveyors?
SS304 is the standard grade offering excellent corrosion resistance for general food and industrial applications. SS316 (or 316L) contains added molybdenum, providing superior resistance to harsh chemicals, acids, and saline environments, making it ideal for pharmaceutical and chemical cleanrooms.
Are these conveyors suitable for high-temperature applications?
Yes. While standard models operate up to 120°C, our specialized high-temperature configurations use heat-resistant solid steel belts, specialized insulation, and high-temp bearings to withstand baking, drying, and thermal processes up to 400°C.
How do you clean and maintain a sanitary stainless steel belt conveyor?
Our conveyors feature crevice-free TIG welding and smooth polished surfaces that support high-pressure water washdowns and clean-in-place (CIP) protocols. Quick-release tension mechanisms also allow fast, tool-free belt inspections.
Can these systems be customized for inclined or curved layouts?
Absolutely. We provide fully custom layout engineering, including inclined/declined elevation changes, side-guiding rails, and specialized flight attachments to match your specific factory floor plan.
CONTACT
WhatsApp:+86 18339211009
Email:sale@xxdahan.com
Add:China, Henan Province, Xinxiang City.Yanjin county forest park gate to the west 1000 meters north road